01
Hot forging
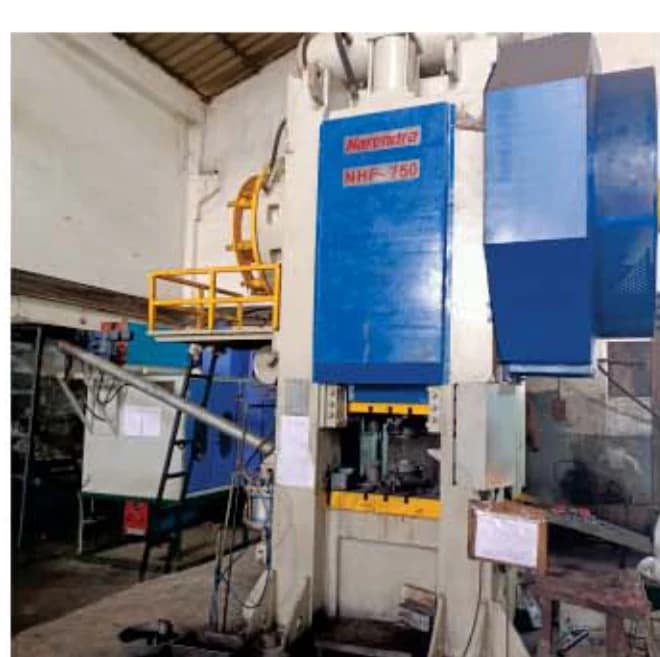
750 T & 450 T hammer presses
Two hammer presses of 750 and 450 tonnes take billet to near-net shape, so the grain follows the part instead of being cut across it.
Infrastructure
Forging, machining and finishing run across the group's units in Rohtak, backed by an in-house lab for hardness, XRF, salt-spray, torque and profile checks.
Every part moves through the same sequence, and the test certificate travels with the box.
Hot forging
750 T & 450 T hammer presses
Two hammer presses of 750 and 450 tonnes take billet to near-net shape, so the grain follows the part instead of being cut across it.
3 × presses · 4 × bolt makers · part former
Three 450 tonne cold presses, four National bolt makers and a Sakamura part former shape fasteners cold and to size, holding strength and finish without removing metal. Automatic thread rolling and tapping finish the thread.
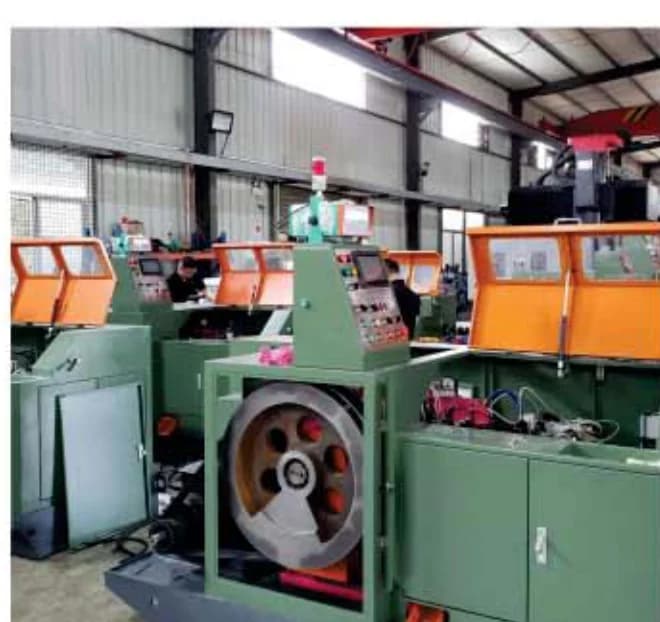
25 × CNC lathes · 5 × VMC
Twenty-five CNC lathes and five vertical machining centres turn and mill to your drawing, batch after batch.
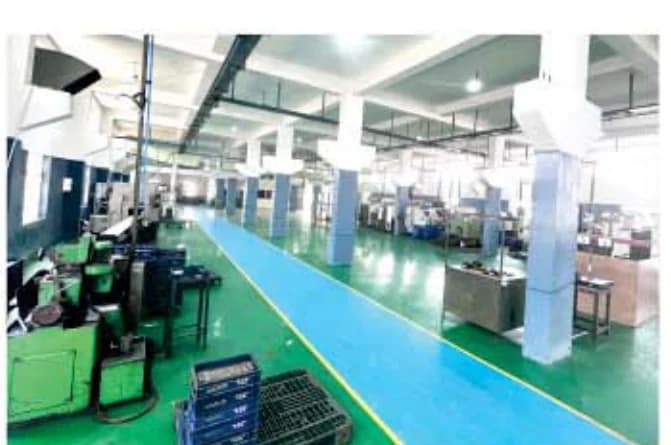
Fully automatic line · RoHS
Fully automatic zinc flake coating applied in-house, then proven in our own salt-spray chamber. Pre-applied thread-locking patch to your specification.
In-house lab
Hardness, roughness, profile projector, air gauge, XRF, coating thickness, salt spray to ASTM B117. All in our own lab. The certificate travels with the box.
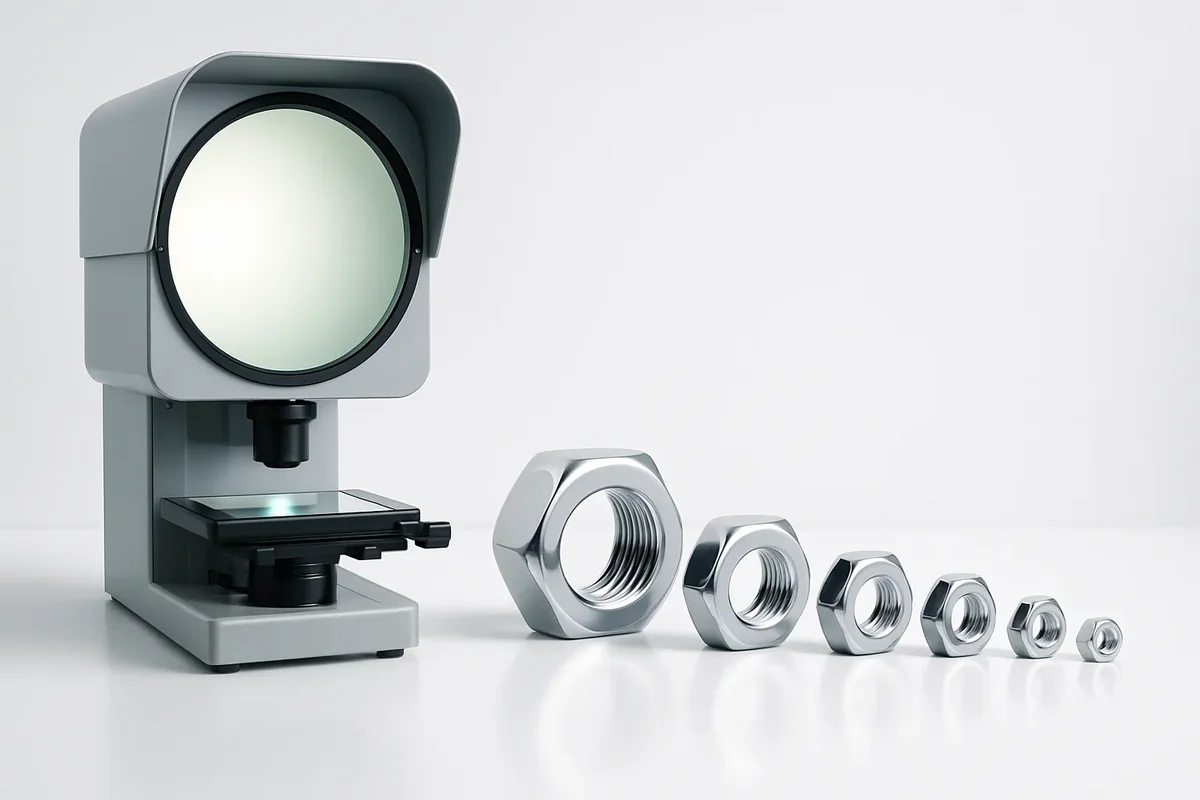
The systems OEM vendor teams audit for are already in place, backed by an in-house lab of hardness, XRF, salt-spray, torque and profile instruments.
Certificate copies shared on request for vendor onboarding.
Upload your part drawing and engineering will come back with feasibility, tooling and lead time.
Replies within one working day